Why Is a Smoke Precipitator Important for Industrial Air Filtration?
Industrial smoke is more than a visible haze. Fine particles can travel beyond a stack, settle on nearby surfaces, and enter the air people breathe. The World Health Organization reported that 99% of the global population lived in places exceeding its air-quality guideline levels in 2019. It also estimated that ambient air pollution caused 4.2 million premature deaths that year. The stakes are real.
A Smoke Precipitator, commonly an electrostatic precipitator, removes suspended particles from exhaust by electrically charging them and collecting them on plates. The U.S. Environmental Protection Agency’s Air Pollution Control Cost Manual describes electrostatic precipitators as capable of very high particle-collection efficiency, often above 99% in suitable applications. Actual performance depends on particle properties, gas conditions, equipment design, and maintenance. A headline efficiency alone can mislead.
Public-health expert Dr. Maria Neira has called air pollution “the new tobacco.” Her warning concerns pollution’s health burden, not a specific machine. That distinction matters. A precipitator can reduce particulate emissions, but it does not automatically control every gaseous pollutant, and poor upkeep can weaken results. In practice, operators should match equipment to the process, inspect collection surfaces, and verify performance with emissions measurements. Dust buildup, changing fuel, or a damaged component may seem minor; each can affect capture. There is no universal setting. This guide explains why a Smoke Precipitator matters, what it can—and cannot—control, and which operating details deserve careful attention.
What a Smoke Precipitator Is: Electrostatic Removal of Industrial Particles
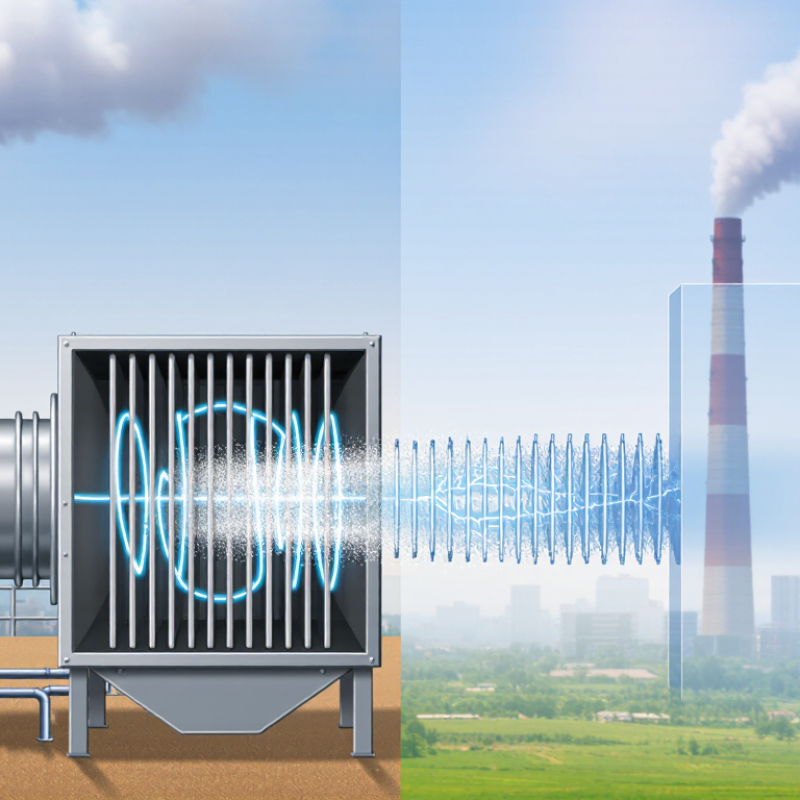
A smoke precipitator is an electrostatic device that removes fine particles from industrial air. It is often called an electrostatic precipitator. Unlike a simple mechanical filter, it uses electrical forces to capture airborne smoke, dust, and oily mist. The process begins when discharge electrodes give particles an electrical charge. These particles then move toward grounded collecting plates. A thin layer forms on the plates and is removed through shaking, scraping, or liquid washing.
This method can handle large air volumes with relatively low pressure loss. That matters in furnaces, metalworking areas, food-processing plants, and other busy facilities. In practical maintenance work, plate spacing, electrode condition, and airflow balance strongly affect performance. A small buildup on an electrode can create unstable sparking. Poor cleaning can reduce collection efficiency before workers notice visible smoke. Regular inspections, airflow measurements, and particle testing provide more reliable evidence than appearance alone.
It is not a perfect solution. Very small particles may escape, especially when voltage settings or gas conditions are unsuitable. Moisture, temperature, and particle resistance also influence electrical capture. Operators should follow engineering standards and use calibrated monitoring equipment. Personal observations can help, but they should not replace documented testing. Even experienced teams may overlook leaks around access doors or damaged seals. A well-designed smoke precipitator works best as part of a complete ventilation system, with safe controls and disciplined maintenance.
Why Capture Efficiency Matters: EPA Reports ESPs Can Exceed 99%
Electrostatic precipitators (ESPs) matter because industrial exhaust can carry fine dust deep into the respiratory system. Their value depends on capture efficiency, not appearance. EPA’s Electrostatic Precipitator Fact Sheet reports typical particulate collection efficiencies of 99% to 99.9%. EPA’s Air Pollution Control Cost Manual also identifies ESPs as high-efficiency controls for large industrial sources.
A 99% result sounds nearly perfect. It is not. For every 10,000 particles entering, about 100 may still leave. At 99.9%, roughly 10 particles remain. That difference becomes significant during continuous operation. A cement kiln, boiler, or metal furnace may process thousands of cubic meters of gas hourly. Small losses can become substantial annual emissions.
Real performance depends on particle size, gas temperature, electrical resistivity, and electrode condition. Moisture changes can help or hurt collection. Poor rapping may allow dust buildup on plates. Field inspections often reveal uneven ash layers, damaged discharge wires, or leaks around access doors. These details are easy to overlook. They also reduce actual efficiency.
EPA data supports strong ESP performance, but reported values are not automatic guarantees. Operators should compare inlet and outlet particulate measurements, pressure trends, and maintenance records. Continuous monitoring provides better evidence than a single commissioning test. A practical review should question the 99% claim, especially when operating conditions change. Capture efficiency is a moving target.
Where Industrial Precipitators Control Particulate Emissions
Why Is a Smoke Precipitator Important for Industrial Air Filtration?
Industrial precipitators control particulate emissions where high-temperature exhaust carries dust, ash, or metal particles. Common locations include cement kilns, steel furnaces, power plants, mineral processing lines, and waste treatment systems. An electrostatic precipitator charges airborne particles and collects them on grounded plates. Rappers then remove the accumulated dust into sealed hoppers. Wet precipitators use liquid droplets instead, helping capture sticky particles and some acid mist.
The strongest value appears at the emission-control stage, before filtered gas reaches a stack. A well-designed unit can reduce visible haze and protect nearby workers, equipment, and surrounding communities. However, performance is not automatic. Gas temperature, moisture, particle resistivity, airflow, and plate cleanliness all matter. Small air leaks can reduce collection efficiency. That detail is often missed.
Tips: Measure pressure drop, spark activity, outlet dust, and hopper levels regularly. Inspect plates, discharge electrodes, seals, and ash-handling equipment during planned maintenance. Keep operating records, because a sudden change may reveal a process problem rather than a filter failure. Do not rely only on clear-looking exhaust. Fine particles can remain invisible. Real facilities are rarely perfect, and maintenance teams should review weak results instead of hiding them.
What Affects Performance: Particle Size, Gas Conditions, and Maintenance
A smoke precipitator is important because it captures fine particles before they enter the workplace or outdoor air. Its performance depends heavily on particle size. Larger particles usually collect more easily, while very fine particles may pass through or require longer treatment time. A visible gray haze can therefore hide a serious filtration problem. Testing should include particle measurements, not only visual inspection.
Gas conditions also change collection efficiency. High gas velocity can reduce contact time inside the precipitator. Excess moisture may cause corrosion, electrical instability, or deposits on internal surfaces. Temperature matters too, especially when gases cool and condensation forms. In practice, operators should monitor airflow, temperature, humidity, and pressure drop together. One reading rarely explains the whole system.
Maintenance is equally important. Dust buildup on collection plates can weaken performance and increase energy use. Damaged insulators may create electrical faults. Regular cleaning, inspection, and calibration help keep the unit stable. However, a fixed maintenance schedule is not always enough. Dust loads can change after a production adjustment. I have seen operating teams trust old settings for too long. That assumption deserves review. Records should connect cleaning dates with emission readings and process changes. Small warning signs, such as rising pressure drop or uneven voltage, should receive attention before visible smoke appears.